
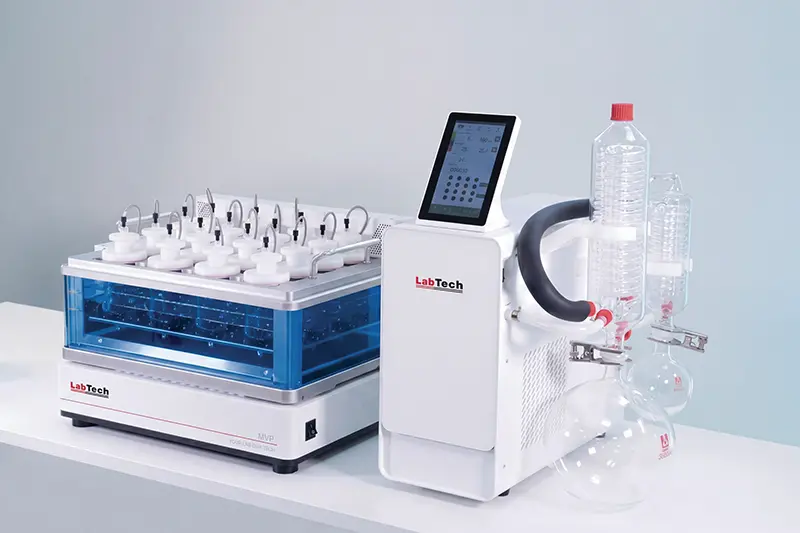


Flex-MVP
The Flex-MVP is a particularly flexible model, suitable for thermosensitive samples. Thanks to its high solvent recovery rate, it allows to reduce the emissions of solvent, proving to be an environmentally friendly concentrator. The Flex-MVP also boasts energy-saving capabilities alongside its main functionalities.
Features and advantages
Super batch processing capability
16 sample positions, compatible with 200ml and 50ml vials
Fully surrounded heating with high evaporation efficiency
The whole sample vial is fully immersed and heated in the water bath
Safe and sample operation
It features a convenient snap-lock safety lock design
Flexible and free access at any time
No need to pause the instrument or pressure relief for all the samples as a single sample can be added and removed at any time
Full transparency
The evaporation chamber is designed with full transparency, providing strong visibility
Independent pipeline to prevent cross contamination
Each sample vessel is sealed and discharged independently through its own pipeline, avoiding liquid transfer issues
User-friendly touch screen control
Designed with a 10’’ touch screen control system
Dual recovery of solvent vapor and exhaust gas
Dual-condenser tower design, enabling dual recovery of solvent vapor and exhaust gas
Shaking bath system
It allows to speed up the evaporation rate. The sample is continuously mixed, preventing the overheating
Exchange top cover system
The MVP Series can use 2 different models of top cover, known as Flex-MVP and MVP-48, making the system more flexible
User-friendly operation
The software allows real-time adjustment of temperature, vacuum and shaking frequency. It supports timed operations and allows for the graphical display of gradient curves and real-time monitoring of all parameters
Flex-MVP EVO
The FLEX MVP-EVO is the advanced evolution of the FLEX MVP, engineered to deliver enhanced performance, greater flexibility and superior operational reliability. Built on the proven capabilities of the FLEX MVP, the EVO version introduces several key technological advantages designed to optimize workflow efficiency and improve end-point detection accuracy in demanding laboratory applications.
Features and advantages
More accurate end-point detection
Featuring an innovative invisible light optical design and independent liquid level sensor, the system ensures reliable light detection with no signal attenuation and strong anti-interference capability.
The End-Point detection process is not affected by particles, bubbles, or sample color, overcoming the accuracy limitations of traditional sensors in complex matrices or high-temperature environments
The End-Point detection process is not affected by particles, bubbles, or sample color, overcoming the accuracy limitations of traditional sensors in complex matrices or high-temperature environments
Independent control, sealing, and sample removal
- Each position is equipped with an independent sealing system. After reaching end-point, the dedicated solenoid valve automatically releases the vacuum of the specific sample, allowing it to be removed individually without affecting other samples. The remaining samples continue running, no need to stop the system or release the overall vacuum.
- All 16 positions are independently controlled, and users can freely select running positions through the software interface.

MVP-12
The MVP-12 is specially produced for large volume needs: up to 12 samples with max. 900ml each can be concentrated simultaneously. For this reason, it is suitable for extraction applications. Designed for high throughput, this instrument replaces up to 12 rotary evaporators, saving valuable lab space and resources.
Features and advantages
Large volume and high throughput
Supports the simultaneous concentration of up to 12 samples, each up to 900 mL
Prevention of cross-contamination
Independent airflow pathways for each sample prevent backflow caused by sample bumping, ensuring reliable results
Efficient concentration
Surrounding water bath heating ensures high thermal efficiency for rapid concentration
High solvent recovery
The solvent recovery rate for 500 ml of petroleum ether is over 85%
Optimized upper cover
The cover includes an upgraded heating function to prevent condensation. Flow path upgraded to Tesla check valve (from PTFE tubing) eliminates cross-backflow, supports heating, and simplifies maintenance
User-friendly operation
Equipped with a safety-lock design, allowing quick, effortless lid opening and secure closing
High concentration efficiency
Fully surrounded water bath heating with higher evaporation efficiency

MVP-48
The MVP-48 automatic parallel vacuum concentrator is a high-capacity and high-efficiency system designed for the rapid evaporation and volume reduction of multiple samples using heating, vacuum, and vortex agitation. Featuring 48 independent positions, it allows up to 48 samples to be concentrated simultaneously using either 60 mL sample bottles or 50 mL centrifuge tubes, providing laboratories with greater flexibility and a more efficient workflow. Widely used in food, environmental and agricultural product testing, the MVP-48 combines high concentration efficiency, user-friendly operation, and environmentally friendly performance to meet the demands of high-throughput laboratories.
Features and advantages
High throughput
Supports simultaneous concentration of up to 48 samples
Flexible compatibility
Accommodates both 60 mL sample bottles and 50 mL centrifuge tubes with elastic sealing lids
User-friendly operation
Features a safety-lock design for easy and safe one-handed lid operation
Prevention of cross-contamination
Each channel is independently sealed and controlled, eliminating accidental cross-contamination between samples
Optimized upper cover
The cover includes an upgraded heating function to prevent condensation. Flow path upgraded to Tesla check valve (from PTFE tubing) eliminates cross-backflow, supports heating, and simplifies maintenance
User-friendly operation
Equipped with a safety-lock design, allowing quick, effortless lid opening and secure closing
High concentration efficiency
Fully surrounded water bath heating with higher evaporation efficiency
A complete package
The MVP Vacuum Concentrator combined with the LabTech Water Chiller delivers an all-in-one evaporation package optimized for high solvent recovery and maximum throughput.

Sample positions
Sample volume
Individual sample adding/removing
Shaking bath
Shaking rpm range
Temperature range
Integrated Android controller
Power consumption
Power supply voltage
End point detection
Dimensions (WxDxH)

Flex-MVP EVO
Sample positions
16
Sample volume
200ml or 50ml concentration cup
Individual sample adding/removing
✓
Shaking bath
✓
Shaking rpm range
0-300 rpm
Temperature range
From room to 70°C
Integrated Android controller
✓
Power consumption
1,8 kW
Power supply voltage
230V 50/60Hz
End point detection
✓
Dimensions (WxDxH)
78x47x55 cm

Flex-MVP
Sample positions
16
Sample volume
200ml or 50ml concentration cup
Individual sample adding/removing
✓
Shaking bath
✓
Shaking rpm range
0-300 rpm
Temperature range
From room to 70°C
Integrated Android controller
✓
Power consumption
1,8 kW
Power supply voltage
230V 50/60Hz
End point detection
✕
Dimensions (WxDxH)
78x47x55 cm

MVP-12
Sample positions
12
Sample volume
900ml concentration cup
Individual sample adding/removing
✕
Shaking bath
✓
Shaking rpm range
0-300 rpm
Temperature range
From room to 70°C
Integrated Android controller
✓
Power consumption
1,8 kW
Power supply voltage
230V 50/60Hz
End point detection
✕
Dimensions (WxDxH)
78x47x55 cm

MVP48
Sample positions
48
Sample volume
60ml vial & 50ml centrifuge tube
Individual sample adding/removing
✕
Shaking bath
✓
Shaking rpm range
0-300 rpm
Temperature range
From room to 70°C
Integrated Android controller
✓
Power consumption
1,8 kW
Power supply voltage
230V 50/60Hz
End point detection
✕
Dimensions (WxDxH)
78x47x55 cm
Main Applications
Wherever samples need concentrating, from food and pharma to environment and chemical QC, MVP Vacuum Concentrators deliver fast and reliable results.

Food
Pesticide residues, additives in food, determination of acid in food and extraction.
Pharma
Determination of API, extraction, contaminants and residues.
Environment
SVOC pollutants in soil, solid waste and atmospheric samples, such as organochlorine residues, polycyclic aromatic hydrocarbons.
Chemical
QC of plastics, petrochemical, oil, fats and textile.


